If you’ve ever walked through a fabrication shop, watched a metalworker assemble a structural beam, or even driven over a bridge, chances are you’ve interacted with hot rolled carbon steel—and you’ve seen weldability in action. As a hot rolled carbon steel supplier, I get asked this question all the time: “Why does one grade of steel weld like a dream, and another give welders headaches that last for days?” It’s not random. Weldability isn’t just a buzzword; it’s the make-or-break factor that turns a good steel product into a safe, long-lasting structure, whether that’s a farm fence bracket, a commercial building’s steel frame, or a heavy-duty truck chassis. Over the 12 years I’ve been working with hot rolled carbon steel, I’ve seen firsthand how picking the right grade for a weld job cuts costs, reduces rework, and keeps projects on schedule. Let’s break down weldability by common hot rolled carbon steel grades, why they differ, and what you need to know to make the right call. Hot Rolled Carbon Steel
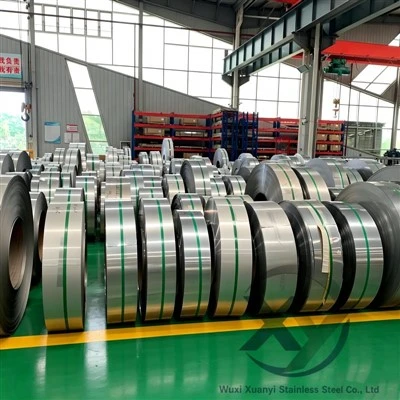
First, let’s get clear on what weldability actually means. For anyone new to the game, weldability is a steel’s ability to be welded without defects—like cracks, porosity, or brittle welds—and still hold up to the load, stress, or environmental conditions it’s meant to handle post-weld. It boils down to three key factors: carbon content (the biggest one for carbon steels), alloying elements that can make steel harder or more brittle, and the steel’s microstructure after it’s hot rolled. Hot rolled carbon steel is made by heating slabs of steel above their recrystallization temperature, then rolling them into sheets, plates, or bars—this gives it a rougher, darker surface than cold rolled steel, but it’s also more affordable, easier to form, and better suited for heavy structural work, which is where most welding happens. The American Iron and Steel Institute (AISI) groups hot rolled carbon steels into four main grades based on carbon content, and each has a totally different weldability profile: low carbon (or mild) steel, medium carbon steel, high carbon steel, and high-strength low-alloy (HSLA) hot rolled carbon steel.
Let’s start with the grade that’s the workhorse of welding: hot rolled low carbon steel, usually with a carbon content of 0.05% to 0.25%. This is the stuff you’ll see in everything from pipe fittings to general structural parts, and it’s the easiest to weld by far. I remember my first big order 10 years ago for a local construction company building a community center; they needed ½-inch hot rolled A36 plates for the beam connections, and their welders finished the job three days ahead of schedule because they didn’t have to preheat the steel or use special filler metal. Why is low carbon steel so weldable? The low carbon content means it’s less prone to a common defect called cold cracking—those tiny, hairline cracks that form in the weld or heat-affected zone (HAZ) when the steel cools too fast. Cold cracking is mostly caused by hard, brittle martensite forming in the HAZ, and martensite needs high carbon content to develop in large amounts. For low carbon steel, even if you run a fast weld, the HAZ stays soft, so no martensite forms. That said, not all low carbon hot rolled steel is identical. A36, the most common structural grade, has a carbon content up to 0.29% max—wait, hold on, that’s just under the 0.3% threshold where weldability starts to dip a little. But even then, A36 is still universally praised for welding; most welders use standard E70 electrodes for shielded metal arc welding (SMAW) or ER70S-6 for gas metal arc welding (GMAW), no preheat needed for thicknesses under ½ inch, and post-weld heat treatment (PWHT) is almost never required. Another low carbon grade, 1018 hot rolled steel, is the go-to for machined parts that also need welding—think of a farmer’s plow bracket that needs to be shaped, machined, then welded to the main frame. 1018 has a carbon content around 0.18%, so it welds just as easily as A36, and it’s more machinable, which is why it’s so popular for custom parts. I always tell customers: if your weld job is basic structural work, general fabrication, or anything where you don’t have extreme load or stress, low carbon hot rolled steel is your safest, most cost-effective bet. The only time you’ll run into issues with low carbon steel is if it has hidden impurities—like sulfur or phosphorus, which make it more prone to porosity or hot cracking (cracks that form as the weld solidifies). That’s why as a supplier, we test every batch of our hot rolled low carbon steel for impurity levels; bad batches of cheap steel can ruin a welder’s day, so we never cut corners on quality.
Next up is medium carbon hot rolled steel, which has a carbon content of 0.30% to 0.59%. This grade is stronger than low carbon steel, so it’s used for parts that need more tensile strength, like axle shafts, gears, and heavy machinery components. But here’s the catch: medium carbon steel’s weldability drops off sharply as carbon content rises. Remember that martensite I talked about earlier? At 0.3% carbon, the HAZ starts forming some martensite if it cools quickly, and that martensite is hard, brittle, and prone to cold cracking. A few years back, I had a customer who bought 1040 hot rolled medium carbon steel (0.40% carbon) to build a small crane boom, and they tried to weld it with the same E70 electrodes they used for A36, no preheat. Within a week, they had three cracks in the welds, and they had to replace the entire boom. That’s the kind of mistake I see happen all the time—people assume all hot rolled steel is the same, but medium carbon needs extra steps. So what do you do to weld medium carbon steel right? First, you need to preheat the steel to 250°F to 400°F before welding—this slows down the cooling rate, so martensite doesn’t form. Second, you need to use a matching filler metal, like E90 electrodes, that has higher tensile strength to complement the steel’s higher carbon content. Third, you might need post-weld heat treatment to relieve residual stresses that build up during welding. Medium carbon steel is still weldable, but it’s not the “weld-and-go” grade that low carbon is. I always warn customers: only use medium carbon hot rolled steel for weld jobs where strength is non-negotiable, and make sure your welders are trained to handle preheating and PWHT. If you don’t have that expertise, it’s better to opt for a lower grade that gets the job done without the extra hassle.
Then there’s high carbon hot rolled steel, with carbon content from 0.60% to 1.00%. This is the hardest, strongest, most wear-resistant hot rolled carbon steel—used for things like springs, railway rails, and cutting blades. But here’s the truth: high carbon steel is very difficult to weld, and most of the time, it’s best avoided for welding applications unless absolutely necessary. The high carbon content makes it extremely prone to cold cracking, even with preheating. I once had a customer who wanted to weld a section of high carbon rail to build a custom workbench top, and after testing a small sample, we told him it would take 24 hours of preheating, specialized filler metal, and constant monitoring to get a good weld, and even then, the joint would only have 60% of the strength of the base metal. He ended up switching to medium carbon steel, which worked perfectly. Why is high carbon steel so hard to weld? It’s not just martensite—high carbon also makes the steel more sensitive to hydrogen embrittlement. Hydrogen from the welding process (from moisture in the electrodes, for example) gets trapped in the weld and HAZ, combining with the high carbon to create cracks that can show up weeks or even months after the weld is done. That’s a huge risk for structural parts, so I never recommend high carbon hot rolled steel for welding projects. If you need a wear-resistant part, there are other options—like hardfacing low carbon steel with a wear-resistant alloy, which is cheaper and more reliable than welding high carbon steel directly. Save the high carbon steel for parts that are formed and machined before use, not welded.
The last main grade is high-strength low-alloy (HSLA) hot rolled carbon steel, which is a middle ground that’s become way more popular in fabrication over the last 20 years. HSLA steel has low carbon content (usually under 0.20%) but is mixed with small amounts of alloying elements like manganese, copper, or vanadium to boost strength without sacrificing weldability. Grades like A572 Grade 50 are the most common HSLA hot rolled steels—they have the same weldability as A36 low carbon steel, but they’re 30% stronger, so you can use thinner plates or bars for the same load, cutting material costs and making projects lighter. That’s a game-changer for industries like trucking and construction, where every pound and every dollar adds up. I supply A572 Grade 50 to a lot of small fabrication shops, and they love it because their welders don’t have to adjust their process at all—same electrodes, no preheat, same speed as A36—but they get a stronger final product. The only thing to watch out for with HSLA steel is the alloying elements; some grades have higher levels of sulfur or phosphorus, which can cause porosity if you don’t set up your welding parameters right. But as long as you follow standard GMAW or SMAW settings, HSLA hot rolled steel is one of the best options for weld projects where you need both strength and ease of welding.
Now, let’s talk about common mistakes that people make with hot rolled carbon steel weldability, because even if you pick the right grade, you can mess it up. First, matching filler metal to the base steel is non-negotiable. Using E70 electrodes on medium carbon steel will give you a weld that’s weaker than the base metal, which is a safety hazard. Second, ignoring thickness. A ¼-inch A36 plate can be welded without preheat, but a 2-inch A36 thick plate needs preheat to prevent cold cracking, even though it’s low carbon. Third, not accounting for environmental conditions. If you’re welding outside in cold weather (below 50°F), even low carbon steel might need a little preheat, because the cold ambient temperature makes the weld cool too fast. Finally, buying cheap, off-spec hot rolled steel. I’ve had customers come to me after buying steel from a no-name supplier where the carbon content was 0.45% instead of the advertised 0.25%—that’s a disaster for a weld job. As a hot rolled carbon steel supplier, all our products come with material test reports (MTRs) that list exact carbon content, alloy levels, and impurity levels, so you know exactly what you’re working with.
At the end of the day, weldability is all about matching the right steel grade to the right job. If you’re building a small fence or a sign frame, go for hot rolled A36 or 1018 low carbon steel—easy to weld, affordable, and reliable. If you’re building a crane boom or a heavy truck axle, medium carbon 1040 or 1045 can work, but make sure your welders are prepared for preheating and PWHT. Never use high carbon hot rolled steel for welding projects; it’s more trouble than it’s worth. And if you need both strength and easy welding, HSLA A572 Grade 50 is the sweet spot.
I’ve been in this business long enough to know that picking the wrong steel grade for welding leads to rework, delayed projects, and even safety issues. That’s why I always take the time to talk through a customer’s specific project: how thick the parts are, what load they’ll carry, where they’ll be used, and what their welding team’s capabilities are. If you’re working on a weld project with hot rolled carbon steel and you’re not sure which grade to use, don’t guess. Reach out to discuss your requirements, and we’ll help you pick the right grade that saves you time, money, and hassle.
Pipe References
- American Iron and Steel Institute. (2020). Carbon Steel Grades and Weldability Guidelines. AISI Steel Products Manual.
- Kalpakjian, S., & Schmid, S. R. (2019). Manufacturing Processes for Engineering Materials, 7th ed. Pearson Education.
- Lincoln Electric Company. (2021). Weldability of Carbon Steels. Lincoln Electric Welding Handbook, 18th ed.
- Metals Handbook. (2015). Volume 6: Welding, Brazing, and Soldering, 11th ed. ASM International.
Wuxi Xuanyi Stainless Steel Co., Ltd.
Wuxi Xuanyi Stainless Steel Co., Ltd. is one of the most professional hot rolled carbon steel manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale bulk durable hot rolled carbon steel made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room 1207, Building 11, Shengang Metropolis Plaza, No. 299 Fangcheng Avenue, Xinwu District, Wuxi City,China.
E-mail: jscherryxy@163.com
WebSite: https://www.xuanyisteel.com/
